

Abstract
Wafer bonding is a crucial process for fabricating microsystems. Within this study, the polymer parylene was used to establish a low-temperature adhesive wafer bonding process for wafers of 150 and 200 mm diameters. The bonding process was investigated for silicon and glass wafers with different additional coatings including silicon dioxide, silicon nitride, aluminum, and parylene C. Important process parameters such as bonding temperature and time were also investigated and the parylene adhesive was analyzed in detail with respect to its dimensions and type. The performance of the parylene bonding was characterized in different aspects, including mechanical tests, cross-sectional scanning electron microscopy, infrared light transmission, and different hermeticity tests. The reliability of the parylene bonded compounds was also investigated with respect to constant loading, mechanical shocking, and thermal cycling. As a result, the parylene bonding is feasible with various materials and shows high tensile and shear strengths of up to 35 MPa and 80 MPa, respectively. Hermeticity was excellent, with a helium leakage rate lower than 10‒7 mbar∙l s−1. The parylene bonded compounds were proven to feature high reliability. Finally, application of the superior properties of the parylene bonding was demonstrated with respect to the fabrication of different three-dimensional structures.

This is an open access article distributed under the terms of the Creative Commons Attribution Non-Commercial No Derivatives 4.0 License (CC BY-NC-ND, http://creativecommons.org/licenses/by-nc-nd/4.0/), which permits non-commercial reuse, distribution, and reproduction in any medium, provided the original work is not changed in any way and is properly cited. For permission for commercial reuse, please email: permissions@ioppublishing.org.
Sensors realized using MEMS (micro-electro-mechanical systems) enable and sustain ongoing trends such as the Internet of Things (IoT), Smart Systems, Industry 4.0, or Point of Care Diagnosis. When using MEMS for new applications, the requirements with respect to the materials and fabrication processes increase. Wafer bonding is crucial for MEMS fabrication with respect to the realization of closed cavities, their encapsulation and packaging. General requirements on wafer bonding are high mechanical strengths, a high reliability, an excellent hermeticity of the bond interface as well as the compatibility with various established MEMS materials and MEMS processes. Biocompatibility of the used materials and low process temperatures enable applications with thermally sensitive biomaterials. Furthermore, the process should be compatible with complex MEMS structures, such as springs, trenches and movable structures, which particularly should not get blocked. Considering the forecasted growth of the global MEMS market from $ 11.5 billion in 2019 to $ 17.7 billion in 2025, 1 also aspects of mass production such as the process compatibility with large and industry standard wafer sizes as well as the process time are important.
In order to fulfill these requirements, this study shows the development and experimental characterization of an adhesive wafer bonding process by using parylene as an intermediate layer between the wafers. Parylene (Poly[p-xylylene]) refers to a family of thermoplastic polymers, which combine a variety of excellent properties. These include chemical inertness against all common acids, bases and solvents, optical transparency, a good mechanical strength as well as ISO 10993 certified biocompatibility and biostability. Furthermore, it shows a comparably good temperature stability with 125 °C and 200 °C long-term and temporary peak temperature in air, respectively. The barrier properties of parylene against gases and moisture enable an almost hermetic sealing. 2–7 These properties cause a good compatibility of parylene with established microsystem technologies, and hence, parylene becomes more and more common in the field of MEMS and MOEMS. 5–7 Due to the possibility to pattern it by using oxygen plasma, 8 the realization of complex structures using bonding and patterned parylene adhesive is possible. In addition, caused by its softness, a parylene adhesive can be advantageous for balancing coefficient of thermal expansion (CTE) mismatches when bonding different materials.
In contrast to other established polymer adhesives for wafer bonding, parylene layers are deposited from the gas phase by the Gorham chemical vapor deposition (CVD) process. Its chemical reactions taking place during the process flow are depicted in Fig. 1a and consist of three steps: first, a commercially available dimer powder is sublimed at temperatures >100 °C. Second, the obtained gas is pyrolytically cracked into monomers at temperatures >550 °C. In the third step, linear polymer chains are formed from the monomer gas in a condensation like reaction at ambient temperatures. The whole process is carried out in vacuum. 2,4–7 In contrast to other polymer adhesives for wafer bonding, such as SU8 photoresist and Benzocyclobutene (BCB), this CVD process enables highly 3D conformal, homogeneous and thin parylene layers, which are free of any intrinsic stresses. Depending on the substituents in the chemical composition of parylene, different parylene types can be distinguished. The chemical formulas of parylene N and parylene C, which are used in the presented study, are given in Figs. 1b and 1c.
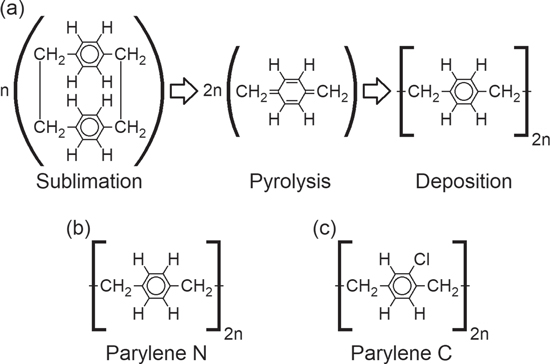
Figure 1. Chemical structures for the three different phases of the Gorham parylene CVD process (a) as well as the chemical structure of parylene N (b) and parylene C (c). 2 .
Download figure:
Standard image High-resolution imageIn the literature, some studies are available, which prove that adhesive wafer bonding based on parylene is feasible. Table I summarizes these publications including the parameters used for bonding as well as the performance of the bonds.
Table I. Comparison of the scientific state of the art for parylene based adhesive wafer bonding.
| Authors/References | Ciftlik et al. 9,10 | Yen et al. 11 | Shu et al. 12 | Kim et al. 13–15 | Ziegler et al. 16 | Noh et al. 17,18 | Poenar et al. 19 | Jang et al. 20 |
|---|---|---|---|---|---|---|---|---|
| Surface of bonding partner 1 | P | P | Si / P | P | P | P | G/P | SiNx/P |
| Surface of bonding partner 2 | SiO2 9 | |||||||
| SiNx 10 | P | P | P | G / P | P | G | SiNx | |
| Wafer diameter [mm] | 100 | N/A | 100 | 100 | 50 | 75 | 100 | 100 |
| Parylene type/thickness [μm] | C 10 | C 5 | N/A 5–10 | N/A <0.381 | N/A 10 | N/A 2 | C 2.5–4 | C 0.05 − 0.2 |
| Patterned | yes | no | no | N/A | no | no | yes | yes |
| Bonding tem-perature [°C] | 280 | 170 | 230 | 130–230 | 160 | 160–200 | 350 | 250 |
| Bonding time [min] | 40 | 30 | 30 | 30 | 30 | 30 | 30 | 480 |
| Bonding force/Contact pressure | 800 N 9 0.1 MPa 10 | 1.5 MPa | 1000 N | 800 N | 4.9 MPa | 1.5 MPa | 1000 N | > 0.5 bar |
| Bonding strength [MPa] | 10 9 23 10 (tens.) | N/A | 1.64–2.38 (tens.) | <4 (tens.) | N/A | 9.16 (tens.) 12.68 (shear) | N/A | 3 (tens.) |
| Remarks | 90% yield; O2 plasma for P acti-vation 10 | — | with oxygen plasma | — | bonded in air, bonded cavities | heated by micro waves | — | heated for 6 h in air at 200 °C before bond |
Abbreviations used: parylene (P), silicon (Si), silicon dioxide (SiO2), silicon nitride (SiNx), glass (G), tensile (tens.)
In summary, parylene bonding was tested on wafers up to diameters of 100 mm and with limited material combinations only. Furthermore, the mechanical strengths of the compounds were comparably low with a maximum tensile strength of 10 MPa. 9 Only one study reports a tensile strength of 23 MPa. 10 Some bonding process in literature also require an activation of the parylene before bonding. 10,12,20 Within two studies, the bonding mechanism and selected properties of the bonded compounds were investigated: Doing so, chain entanglement is suggested as the main principle for the realization of a parylene bond. Furthermore, the compounds were tested with respect to aging and long-term compatibility with chemicals. As a result, aging of the compounds for two years did not affect the compounds negatively. But long-term storage in chemicals harmed the bonding, however, the mechanical strengths of the bonds were initially already very low with a tensile strength of <4 MPa. 13,15
The presented study aims to progress the parylene adhesive wafer bonding into an industry suitable process for the highly reliable bonding of wafers with diameters of 150 mm and 200 mm, respectively. Doing so, first, the material compatibility of parylene C with the bonding process conditions is investigated. Next, relevant bonding parameters such as bonding temperature, bonding time and contact pressure are investigated and optimized with the aim to realize a bond of good mechanical stability. For this, the tensile and shear strengths of the bonds are measured. Subsequent to this, the transferability of the obtained results to various material combinations is tested. In the next step, the requirements on and the dependencies of the parylene adhesive are analyzed with respect to the geometries, dimensions and type of parylene. Then, the bond interface of parylene bonded components is investigated by scanning electron microscopy (SEM) analysis of cross-sections and infrared (IR) light transmission imaging. Also, the hermeticity of the bond is determined by different methods and the reliability of the bonds with respect to continuous mechanical loads, mechanical shock testing and thermal cycling is measured. Finally, the performance of the parylene adhesive wafer bonding for different application scenarios is studied.
Experimental
Compatibility of parylene C with bonding process conditions
Though parylene based adhesive wafer bonding is reported in scientific literature, 9–20 no investigations were performed about the impact of the bonding process conditions on parylene. Hence, within a first experiment, the potential impact of the bonding process conditions on the chemical stability of parylene C was determined using Fourier transformed Infrared spectroscopy (FTIR). Doing so, free-standing parylene C membranes were fabricated following the process flow described in annex A (Fig. A·1). These membranes were annealed in a vacuumed chamber for 30 min at different relevant bonding temperatures of 260 °C, 280 °C, 300 °C, and 320 °C to simulate the conditions of the parylene wafer bonding process. These temperatures were chosen since they are slightly below and above the melting point of parylene C at 290 °C. 3 Before and after annealing, the parylene C membranes were measured in a VERTEX 70 FTIR spectrometer (Bruker corporation), using a wave number k range of 3100 cm−1 to 700 cm−1. Due to constructive and destructive interferences caused by the measurement setup in transmission mode, the obtained spectra featured a superposition with a sinus curve. In order to remove this sinus and smooth the spectra, the data were mathematically processed as described in 21 in detail. Briefly it can be summarized by fitting the sinus according to Eq. 1, whereas I is the intensity [a. u.], λ [μm] is the wave length, k is the wave number [cm−1] and A, B, C, and D are constants to be fitted, followed by subsequent subtraction of the fitted function from the original data.
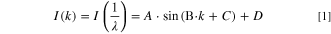
Since the relevant temperature range includes temperatures close to or above the melting point of parylene C, 3 in addition to the FTIR investigations on the membranes, the potential change of the dimensions due to softening and liquefying of the Parlylene was investigated. Doing so, parylene C structures of 200 μm width were prepared on a silicon wafer and annealed at the different temperatures and conditions given above. After annealing, the width of the test structures was measured by light microscopy again.
Wafer processing for sample preparation
The preparation of the samples for the parylene based wafer bonding is schematically presented in Fig. 2. Doing so, double side polished silicon wafers (Siegert Wafer GmbH) of 150 mm diameter (6’) and 625 μm thickness were used for the wafer with the parylene structures (wafer 1). After cleaning, a 500 nm silicon dioxide was deposited on both sides by thermal oxidation (2). The backside silicon dioxide was patterned into frames using a mask of photoresist and wet chemical etching in hydrofluoric acid solution. Next, the structures of the silicon dioxide were transferred into silicon by a 2 μm deep etch in 30% potassium hydroxide at 80 °C for about 2 min (3). Note that the described process for the backside patterning was used only for the samples to enable dicing after bonding and can be replaced by any other method, which enables an accurate alignment for dicing such as transferring marks on the backside or using other patterning methods (dry etching). Particularly, this process does not cause a general incompatibility of the Parylene bonding process with CMOS processing. After the described patterning process (3), the backside was masked and parylene C was deposited (4) following the described CVD Gorham process using a Parylene LC 300 RW lab coater (Plasma Parylene Systems GmbH) and temperatures of 130 °C and 740 °C for sublimation and pyrolysis, respectively. After removal of the backside masking, the parylene was patterned into frames (5) with the same design as the backside silicon dioxide and silicon patterning, respectively, using oxygen plasma etching and a mask of photoresist. A scheme of the parylene frames is depicted in Fig. 3. The symmetric pattern of the front side (parylene) and backside (silicon and silicon dioxide) enables an accurate dicing after bonding. Alternatively, for some experiments borofloat glass wafers (Siegert Wafer GmbH) with the same diameter and a thickness of 500 μm were used instead of silicon wafers (wafer 1). Due to the transparency of glass, only the coating of parylene on the front side and subsequent patterning (steps (4) and (5), respectively) were performed on these wafers.
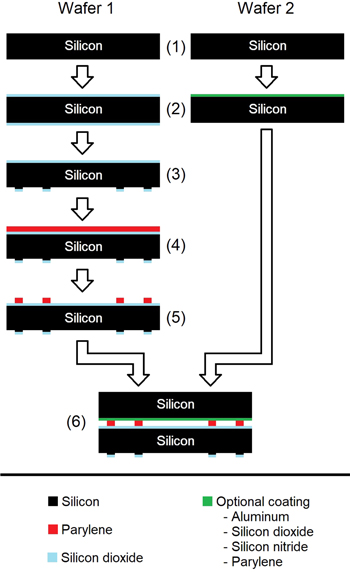
Figure 2. Schematic process flow for the preparation of the wafers before adhesive bonding (1) to (5) and the subsequent parylene bonding (6). Note that the graphic is not to scale.
Download figure:
Standard image High-resolution image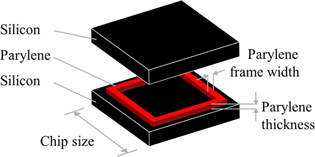
Figure 3. Test structures for the evaluation of the parylene adhesive wafer bonding process.
Download figure:
Standard image High-resolution imageFor the second wafer (wafer 2), a single side polished silicon wafer of 150 mm diameter and 675 μm thickness was used. For some experiments, this wafer was coated with an additional layer such as aluminum, silicon dioxide, silicon nitride, or parylene C. Finally, both wafers were bonded (6) using a SB8 substrate bonder (SÜSS MicroTech SE), different bonding parameters and parylene geometries as described in the following chapters. All bonds were carried out in vacuum conditions (<10−3 mbar). Some experiments were repeated on silicon wafers with a diameter of 200 mm (8″).
Determination of yield and mechanical characterization
In order to investigate the mechanical stability of the parylene bonded compounds as well as the influence of the bonding parameters, materials, parylene dimensions and type as well as aspects of reliability, the tensile strength and the shear strength were determined. Doing so, the bonded wafers were diced into chips according to the size of the bonding frames. After dicing, the yield was determined by the ratio of the number of chips still being bonded to the total number of bonding frames on the wafer. For each mechanical test, a total number of ten chips were collected from positions at the wafer center, at half radius and at the edge. The measurement of the mechanical strengths was performed using a TIRA 2805 equipped with a force sensor with a nominal load of 1 kN and a sensitivity of 2 mV/V. For the preparation of the tensile test, a stainless steel stud was glued on both sides of the chip compound using liquid cyanacrylate glue (Pattex). For the tensile test, the pulling force was measured in dependency of displacement and time, using a test speed of 3 μm s−1 and a pre-force of 5 N. The shear test was performed without any additional sample preparation, using the same equipment and shearing the samples at an angle of 180°. Subsequent to the mechanical tests, optical microscopy was used to investigate the fracture surface, determine the bonding area and, hence, calculate the tensile and shear strength, respectively.
Bonding parameters
For understanding the parylene adhesive wafer bonding process and identifying a suitable parameter range, bonding processes were performed varying the contact pressure, the bonding temperature and the bonding time, respectively. All investigations were performed on silicon—silicon compounds (Si-P-//-Si) using patterned parylene C frames of 5 μm height and 200 μm width and a chip size of 5 × 5 mm2. The contact pressure was varied between 0 bar (no additional contact pressure beside the wafer mass), 1 bar, 2 bar and 3 bar tool setting. Doing so, the bonding time and temperature were kept constant at 10 min and 300 °C, respectively.
The bonding temperature was varied between 260 °C, 280 °C and 300 °C, whereas the latter two temperatures were chosen to be slightly below and the third one slightly above the melting point of parylene C. 3 The lowest temperature of 260 °C was selected in order to investigate, if the bonding temperature can be reduced. All investigations with respect to the bonding temperature were performed using silicon-silicon compounds (Si-P-//-Si) and silicon-glass (Si-//-P-G) compounds additionally, to verify the tendencies are independent of the used materials.
Finally, the bonding time was varied between 5 min, 10 min and 30 min, respectively, keeping a constant contact pressure of 2 bar and a bonding temperature of 280 °C.
Bonded materials
For the investigation of the compatibility of the parylene adhesive wafer bonding with different materials relevant for MEMS technology, the bonding partner (wafer 2 in Fig. 2) was coated with additional layers. These include 500 nm thermal silicon dioxide (Si-P-//-SiO2-Si), 100 nm low pressure CVD coated silicon nitride (Si-P-//-SiNx-Si), 200 nm sputtered aluminum (Si-P-//-Al-Si) and 2.5 μm parylene C (Si-P-//-P-Si). Additionally, the wafer 1 (see Fig. 2) was replaced by borofloat glass substrate (Si-//-P-G). With respect to the realization of optical devices based on the transparency of parylene and glass, the parylene was considered to be deposited and patterned on the glass wafer instead of the silicon wafer. All bonds were performed with patterned parylene C bonding frames of 200 μm width and 5 μm height.
Dimensions of the parylene adhesive
The dimensions of the parylene adhesive were varied with respect to the height and the width of the bonding frames (see Fig. 3). Table II summarizes the samples used for this investigation with respect to their frame width, parylene thickness, chip sizes and number of chips (bonding frames) on each wafer.
Table II. Dimensions of the parylene C frames used for parylene bonding.
| Parylene frame width [μm] | Parylene thickness [μm] | Chip size [mm2] | Number of bonding frames (maximal chips) per 150 mm wafer |
|---|---|---|---|
| 70 | 5 | 5 × 5 | 440 |
| 200 | 5 | 5 × 5 | 368 |
| 200 | 10 | 5 × 5 | 368 |
| 2000 | 5 | 13 × 13 | 74 |
| Non-patterned (full parylene layer) | 5 | 5 × 5 | 638 |
In a first experiment, the influence of the parylene thickness was determined using silicon-glass bonds (Si-//-P-G) and thicknesses of 5 μm and 10 μm, respectively. The parylene frame width was kept constant at 200 μm as well as the bonding time of 10 min and the contact pressure of 2 bar. The bonding temperature was varied between 280 °C and 300 °C.
Furthermore, the parylene bonding frame width was varied between 70 μm, 200 μm, 2000 μm and non-patterned parylene. Note that the chip size for the 2000 μm wide frames was larger than for the other samples. For this investigation silicon-silicon compounds (Si-P-//-Si) were used, keeping a constant height of the bonding frames of 5 μm and a constant parameters set for the bonding process of 280 °C bonding temperature, 2 bar contact pressure and 10 min bonding time.
Parylene type
Due to its superior properties such as a better temperature stability and hermeticity, 3 parylene C usually is preferred for the usage as an adhesive for wafer bonding. 9,11,19 Since in the literature a lower duration and temporary peak temperature for parylene N is given compared to parylene C, 3 it is aim of this section to investigate, whether parylene N can be used for the adhesive wafer bonding was well, and if applicable even at reduced temperatures.
Doing so, three silicon-silicon compounds (Si-P-//-Si) were bonded with parylene N frames of 5 μm height and 200 μm width. The contact pressure and bonding time remained constant at 2 bar and 10 min, respectively. For comparison with parylene C bonds, bonding temperatures of 280 °C and 300 °C were investigated. Additionally, a reduced bonding temperature of 250 °C was tested.
Cross-sectional analysis of the bond interface
For the characterization of the interface between the parylene C and the bonded partner wafer as well as for analyzing any potential squeezing of the parylene due to the bonding process, cross-sections were prepared and analyzed in the SEM. The preparation of the cross-sections included embedding into epoxy and subsequent grinding. All samples selected for this analysis were silicon-silicon compounds (Si–P–//–Si) bonded with patterned parylene C frames of 5 μm and 200 μm height and width, respectively. To investigate the impact of the bonding temperature on the bonding interface, samples bonded in the previously established temperature range between 280 °C and 300 °C were selected. The bonding time for both was 10 min. However, in order to visualize any potential squeezing of the parylene, for the sample bonded at 300 °C, a compound was selected, which was bonded at 3 bar contact pressure. For the parylene-parylene bonds (Si-P-//-P-Si), the particular interest is focused on the investigation of the bonding interface between the two parylene layers. Hence, the cross-sections of two parylene-parylene compounds samples were analyzed by SEM. Doing so, samples were selected, which were bonded at 280 °C and 300 °C and a constant contact pressure and bonding time of 2 bar and 10 min, respectively.
Infrared light transmission
In order to investigate the bonding quality with respect to homogeneity and the bond interface itself, all wafer compounds of this study were analyzed by infrared (IR) light transmission. Since all successful bonds appeared very similar in the IR light transmission analysis, only two compounds are presented within this paper: A silicon-silicon bond (Si–P–//–Si) with a parylene frame width and height of 200 μm and 5 μm, respectively, as well as one with non-patterned parylene adhesive.
Hermeticity
The hermeticity of the parylene bond interfaces was investigated in two setups. First, the previously described structures with parylene C were used to realize sealed cavities. To enlarge the volume of the cavity, the bonded wafer was etched at the location of the later cavity for a depth of 200 μm. Using thin wafers of 300 μm thickness only, the etching caused the side effect of realizing a remaining silicon thickness of 100 μm, which can be used as bendable silicon membranes. The width and height of the parylene bonding frame was 100 μm and 5 μm, respectively. For the bonding, a contact pressure of 2 bar, a bonding time of 10 min and bonding temperatures of 280 °C and 300 °C were applied. Due to performing the bonding process in vacuum, the cavities were vacuumed after bonding. The vacuum in the cavity caused a deflection of the silicon membrane, which was measured for 40 days using white light interferometry. Moreover, the samples were used to perform a standardized helium leakage test in accordance to MIL-STD-883. Doing so, after bonding and dicing, the chips were stored in a helium atmosphere at 1 bar overpressure for one week (bombing). In case of any leakages, the helium penetrates into the cavities. In order to measure the helium leakage rate, after the bombing, the chips were placed into a vacuum chamber, which was connected to a mass spectrometer. The helium leakage rate was recorded every ten seconds. The remaining helium in the spectrometer was compensated by reference measurements without samples in the chamber, which were subtracted from the measurement results.
For a second investigation of the hermeticity of the parylene bond interface, a capacitive MEMS acceleration sensor was used. The details of the sensor structure can be found elsewhere 22–24 and can be briefly summarized: An acceleration causes a deflection of a movable and suspended seismic silicon mass, which is placed in a sealed cavity. The seismic mass is connected to movable electrodes of a capacitor. Hence, the capacitance of the MEMS acceleration sensor changes depending on acceleration. The relevant feature of this sensor with respect to the investigation of the hermeticity of the bond interface are the vibration characteristics of the seismic silicon mass (natural frequencies), which strongly depend on the vacuum in the cavity of the seismic mass. Air or any other gas in the cavity is damping the vibration of the seismic mass and, hence reduces the natural frequency of the sensor. For the characterization of the hermeticity of the parylene bond interface, the described MEMS acceleration sensor is sealed by different parylene bonding frames of 50 μm and 200 μm width, respectively, and a height of 5 μm each. The bonding parameter set was chosen to be a bonding temperature of 300 °C, a contact pressure of 2 bar and a bonding time of 30 min. For the quantification of the vacuum inside the cavity, the frequency characteristics, namely the −3 dB frequency was measured after bonding and over a time. For reference, the −3 dB frequency was measured before bonding at ambient pressure (1 bar) as well. Furthermore, for reliability testing of the hermeticity, some samples were thermally cycled as described in the reliability section.
Reliability
The reliability of the parylene bonded compounds was investigated for several aspects. For the thermal reliability, silicon-silicon (Si–P–//–Si) and silicon-glass compounds (Si-//-P-G) were thermally treated for 100 cycles. Each cycle consisted of annealing at 125 °C for 30 min and subsequent cooling to −40 °C for another 30 min. The samples were bonded by a parylene frame of 200 μm width and 5 μm height using a bonding time of 10 min, a contact pressure of 2 bar and a bonding temperature of 280 °C and 300 °C, respectively. After the thermal cycling, the chips were mechanically characterized by a tensile test and compared with the results of non-cycled chips from the same wafer.
For the investigation of the mechanical reliability, silicon-silicon compounds (Si–P–//–Si) bonded by a 200 μm wide and 5 μm high parylene C frame at a bonding temperature of 300 °C, a bonding time of 10 min and a contact pressure of 2 bar were used. For a first group of ten samples, a continuous load of 3 kg (∼30 N) was applied for 100 h. A second group of 20 samples was mechanically shocked by gluing them on a stainless steel plate, which was dropped from a height of 1 m. Using an acceleration sensor, the average mechanical shock was determined to be 918 g ± 44 g (gravity constant g = 9.81 m s−2). Out of the 20 samples, ten were mounted horizontally so that the impact of the mechanical shock was perpendicular to the bonding interface. The other ten samples were mounted vertically so that the mechanical shock was parallel to the bonding interface. A third group of ten samples was naturally (non-accelerated) aged at ambient conditions for 700 days. Finally, all samples were characterized by tensile test and the results were compared to the values after bonding.
Bonding with structures
The parylene adhesive wafer bonding was investigated for two types of three-dimensional (3D) structures and applications, respectively. Within a first structure, the ability of parylene to level 3D structures was tested. Doing so, aluminum electrodes with a height of 100 nm to 1 μm and a width of 5 μm to 200 μm were patterned on the partner wafer to be bonded to. The bond was performed with non-patterned parylene of 5 μm thickness at a bonding temperature of 300 °C, a contact pressure of 2 bar and a bonding time of 10 min. After the bonding, cross-sections were prepared by dicing, embedding into epoxy and grinding and were afterwards analyzed by SEM.
Independent of this and using a second 3D structure, the usage of parylene adhesive wafer bonding to realize cavities was investigated. Doing so, a silicon wafer was coated with 1 μm silicon dioxide, which was patterned to realize steps. Finally, on the front side of this wafer, parylene with a thickness of 0.5 μm to 4 μm was deposited, which remained non-patterned. This wafer was bonded against a blank silicon wafer at a bonding temperature of 300 °C. After bonding, again cross-sections were prepared and analyzed by SEM.
In the context of realizing more complex MEMS structures using parylene adhesive wafer bonding, the process compatibility of the compounds with subsequent processes such as grinding and chemical mechanical polishing (CMP) was tested as well.
Results and Discussion
Compatibility of parylene C with bonding process conditions
The fitting parameters for the sinus function according to Eq. 1 are given in table A·I in annex A. The obtained and processed FTIR spectra of the parylene C membranes before and after annealing are depicted in Fig. 4 and are in accordance with the typical FTIR spectra of parylene C reported in literature. 25–29 Furthermore, the spectra show no difference when comparing the data before and after annealing and the different annealing temperatures, respectively. A detailed assignment of the individual peaks can be found in in Table A·II in annex A. It has to be noted that no additional peaks are observed, particularly no peak at 1700 cm−1, which would refer to the oxidation of parylene. 27 Hence, it can be concluded that there is no negative impact of the bonding process conditions on the chemical composition of parylene C.
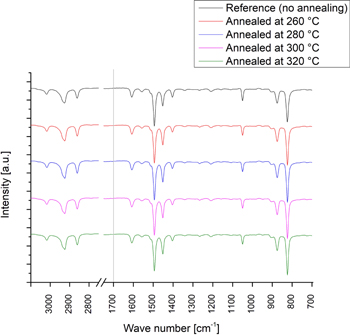
Figure 4. FTIR spectra measured at free-standing parylene C membranes after annealing at temperatures relevant for the parylene based adhesive bonding as well as at not annealed reference.
Download figure:
Standard image High-resolution imageThe width of the 200 μm parylene structures was measured to be within the range of 197 μm to 203 μm for all samples after annealing and hence, is still close to the initial value of 200 μm with a maximal deviation of 3 μm only. Thus, it can be concluded that there is no change of the dimensions during the bonding due to softening or liquefying of parylene C.
Hence, parylene C is compatible with the conditions of a wafer bonding process. This is independent of using bonding temperatures below or slightly above the melting point, up to 320 °C.
Bonding parameters
The results of the mechanical strength of the silicon-silicon (Si-P-//-Si) compounds, bonded at different contact pressures are depicted in Fig. 5. For a contact pressure of 0 bar, no bonding could be achieved. The samples from the bond performed with 1 bar contact pressure were not measurable accurately due to failure of the glue between the chip and the stud. Hence, the compound remained intact after the tensile test. For bonding at a contact pressure of 2 bar, the maximum strengths for no sample failure was 24.2 MPa (tensile) and 68.0 MPa (shear), respectively,whereas the median strengths (50% failure) were 38.7 MPa (tensile) and 88.0 MPa (shear), respectively. When increasing the contact pressure to 3 bar, the maximum strengths for no sample failure changed to 39.8 MPa (tensile) and 64.5 MPa (shear), respectively,whereas the median strengths (50% failure) changed to 50.1 MPa (tensile) and 71.5 MPa (shear), respectively. From the results it can be concluded that at a minimum pressure is required to realize the bonding. Considering the tensile strengths only, it can be suggested that an increase of the contact pressure causes slightly improved mechanical stabilities. However, when considering the shear strengths as well, and the fact the samples bonded at a contact pressure of 2 bar reach slightly higher values then the ones bonded at 3 bar, it can be concluded that the impact of the contact pressure to the mechanical strength is comparably low. Compounds bonded between 2 bar and 3 bar contact pressure feature a good mechanical strength. After dicing, a yield of 100% was observed for the compounds bonded at 2 bar and 3 bar. For the reduced contact pressure of 1 bar, the yield was slightly reduced but still >99%. For all samples, no dependency of the mechanical strength from the position on the wafer was observed.
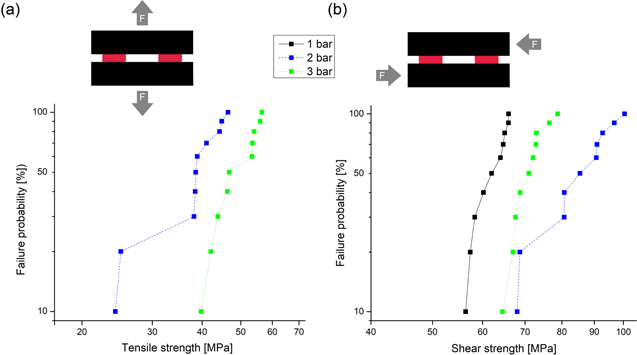
Figure 5. Tensile strength (a) and shear strength (b) of silicon-silicon compounds (Si–P–//–Si) bonded at the indicated contact pressures and 300 °C bonding temperature for 10 min Note that the samples bonded at a contact pressure of 1 bar were not measurable due to glue failure. Detailed values are given in Table C·I.
Download figure:
Standard image High-resolution imageFigure 6 presents the results of the tensile and shear test, respectively, for silicon-silicon (Si-P-//-Si) and silicon-glass (Si-//-P-G) compounds bonded at 260 °C, 280 °C and 300 °C. The tensile strength of the silicon-glass compounds bonded at 300 °C was not measurable due to glue failure. The debonding behavior in the tensile test was observed to be temperature dependent. Samples bonded at 300 °C and, hence, above the melting point of parylene, debonded only adhesively. In contrast to this, the samples bonded at 260 °C and 280 °C debonded adhesively and cohesively. However, in the shear test, all samples debonded adhesively, independent of the bonding temperature. The mechanical tests indicate a strong temperature dependency for both material combinations. Comparing the lowest and the highest bonding temperature of 260 °C and 300 °C, respectively, an increase of a factor of 4 to 5 is observed. The highest mechanical strengths were measured for compounds bonded at 300 °C with average values of 35 MPa and 80 MPa for the tensile and shear strength of a silicon-silicon compound (Si-P-//-Si), respectively. In contrast to this, a bonding temperature of 260 °C produces only a low mechanical stability. Hence, it can be concluded that a good range for the bonding temperature is between 280 °C and 300 °C. Again, the mechanical strength was independent on the wafer position. For all samples, a yield of 100 % was achieved after dicing.
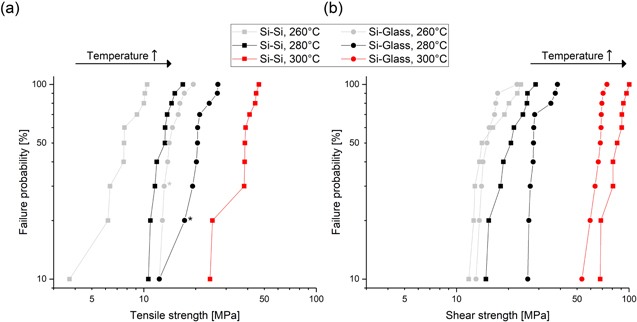
Figure 6. Tensile strength (a) and shear strength (b) of silicon-silicon (Si-P-//-Si) and silicon-glass (Si-//-P-G) compounds bonded at different temperatures and 2 bar contact pressure for 10 min. Note that for the shear strength the silicon-silicon (Si-P-//-Si) compounds and the silicon-glass compounds (Si-//-P-G) have an identical fit. Marks with * indicate glue failure as well. Detailed values are given in Table C·I. 30
Download figure:
Standard image High-resolution imageThe results of the tensile and shear tests for the silicon-silicon compounds (Si-P-//-Si) bonded with different bonding times are depicted in Fig. 7. For all tensile tests, cohesive and adhesive debonding was observed. In contrast to this, in the shear tests, all samples debonded adhesively. Shorter bonding times caused a slightly higher mechanical strength. A possible reason for this could be the impact of the longer annealing time on the crystallinity of parylene. 31,32 However, when considering the average mechanical strength of each bond, the increase of the mechanical strength is given by a factor of ∼1.5 only, comparing a bonding time of 5 min and 30 min. Hence, the bonding time has a comparably low influence on the mechanical stability of the bonded compound. Bonding times between 5 min and 30 min produced good results. Similar results for the time dependency of the mechanical strength can be observed for the bonding of silicon-glass (Si-//P-G). For all samples, the yield was 100 % after dicing and the mechanical strength distribution was independent of position on the wafer.
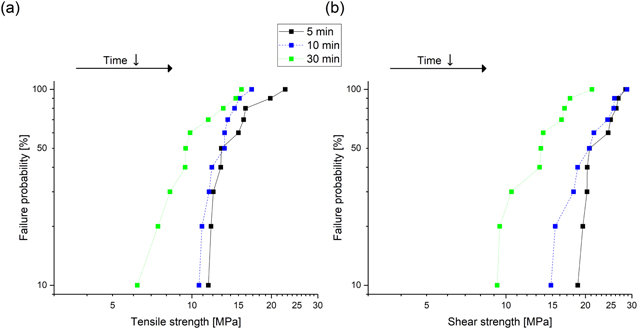
Figure 7. Tensile strength (a) and shear strength (b) of silicon-silicon (Si-P-//-Si) compounds bonded for different times, at a bonding temperature of 280 °C and a contact pressure of 2 bar. Detailed values are given in Table C·I. 30
Download figure:
Standard image High-resolution imageIn summary it can be concluded that contact pressure and bonding time have a low influence on the mechanical stability, whereas the bonding temperature has a comparably high impact. Furthermore, it can be summarized that the yield is excellent and the distribution of the mechanical strength on the wafer is homogeneous. Both parameters are independent of the contact pressure, bonding temperature and bonding time in the tested ranges.
Bonded materials
Figure 8 summarizes the average tensile (a) and shear (b) strengths of the parylene bonded compounds in dependency of the material combination and the bonding temperature. The error bar indicates the standard deviation. Note that for the tensile tests of glass, silicon dioxide, silicon nitride and parylene C, for some samples glue failure was observed. Hence, the real values of the tensile strength are expected to be higher. For all samples, no dependency of the mechanical strength on the wafer position was observed. The yield was 100% for all samples except for the ones bonded at 280 °C against silicon nitride (Si-P-//-SiNx-Si) and aluminum (Si-P-//-Al-Si). For these two samples, the yield was slightly reduced, but still >99%. The results indicate that parylene bonding of the given materials is feasible with good mechanical stabilities, yields and homogeneities. Due to some glue failure during the tensile test, the results of the shear test are considered in more detail. For all materials, the dependency of the mechanical strength on the bonding temperature (280 °C vs 300 °C) was observed as described previously. Doing so, the bonding at a temperature of 300 °C produced the better mechanical stability. It is interesting to note that for a bonding temperature of 280 °C no significant dependency of the shear strength on the material combination was observed (overlapping of the standard deviation ranges of all samples compared to the silicon sample). In contrast to this, for bonding at 300 °C, a silicon dioxide (Si-P-//-SiO2-Si) or silicon nitride (Si-P-//-SiNx-Si) coating slightly reduces the shear strength of the bond. Exchanging the silicon substrate (Si-P-//-Si) to glass (Si-//-P-G) also reduces the shear strength. Comparing bonding of silicon to glass (Si-//-P-G) and bonding against silicon dioxide (Si-P-//-SiO2-Si) and considering the material similarity of glass and silicon dioxide, the results indicate that parylene bonding is feasible for parylene deposited and patterned on these materials, but also for parylene being bonded against these materials. Nevertheless, for all investigated samples, the impact of the material is less than that of the bonding temperature.
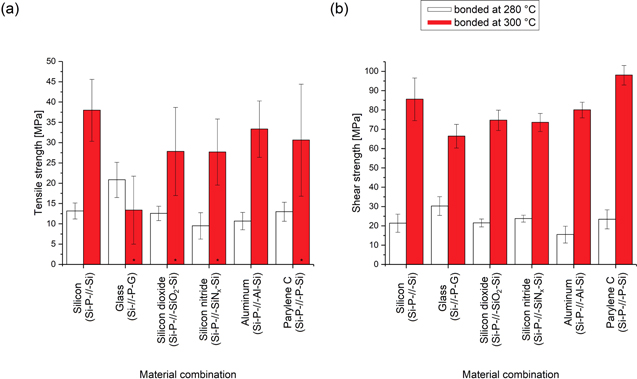
Figure 8. Average tensile strength (a) and shear strength (b) of parylene coated wafers bonded against silicon wafers with different coatings. The bonds were performed at 280 °C and 300 °C, respectively, a contact pressure of 2 bar and a bonding time of 10 min Marks * indicate glue failure of at least one sample. Detailed values are given in Table C·II.
Download figure:
Standard image High-resolution imageDimensions of the parylene adhesive
Figure 9 summarizes the results of the mechanical characterization of the silicon-glass (Si-//-P-G) compounds bonded with 5 μm and 10 μm parylene frames at bonding temperatures of 280 °C and 300 °C. Note, that the tensile strength of the compounds bonded at 300 °C was not measurable due to glue failure. All samples debonded cohesively and adhesively during the tensile test, whereas they only debonded adhesively during the shear test. The yield of all wafer bonds was 100%. For bonding temperatures of 280 °C, only a minor dependency of the mechanical strength on the parylene thickness was observed. Doing so, lower parylene thicknesses caused slightly increased mechanical strengths. The higher impact of the parylene bulk properties at higher thicknesses could be a possible reason for this behavior. In contrast to this, no thickness dependency of the mechanical strength was observed at bonding temperatures of 300 °C. A potential reason for the different behavior could be the bonding below and above the melting point. Additional experiments revealed that also parylene thicknesses as low as 500 nm are sufficient to realize stable compounds. Hence, the parylene thickness suitable for bonding was demonstrated to range from 0.5 μm to 10 μm.
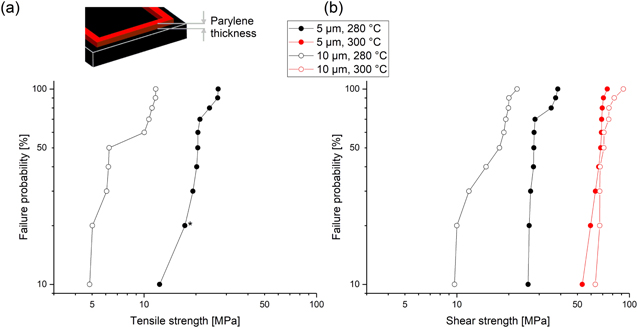
Figure 9. Tensile strength (a) and the shear strength (b) of silicon-glass compounds (Si-//-P-G) with different thicknesses of the parylene frames, bonded at different bonding temperatures. The contact pressure, the bonding time and the parylene frame width were kept constant at 2 bar, 10 min and 200 μm, respectively. Marks with * indicate glue failure. Detailed values are given in Table C·III. 30
Download figure:
Standard image High-resolution imageThe results of the tensile and shear tests, respectively, for the compounds bonded with different parylene frame width are presented in Fig. 10. No dependency of the mechanical strength on the wafer position was observed. The debonding mechanism was determined to be dependent on the parylene frame width: For the tensile tests, the samples with a frame width of 70 μm debonded adhesively. In contrast to this, the samples with a frame width of 200 μm debonded adhesively and cohesively. A similar tendency was observed for the shear tests. Only adhesive debonding was observed for frame widths of 70 μm and 200 μm, whereas samples with larger frame widths debonded in both mechanisms. The results for the variation of the parylene frame width show that parylene adhesive wafer bonding is feasible for a wide range of dimensions, from as low as 70 μm in width to non-patterned parylene. For the mechanical stability of the samples with a parylene frame width of 70 μm, 200 μm and non-patterned parylene, no significant influence of the parylene frame width on the mechanical stability was observed. For the remarkably higher shear strength observed for samples with a parylene frame width of 2000 μm, it has to be noted that the chip size was remarkably larger as well (see Table II). Particularly, the chip size was larger than the stud size. Hence, it is questionable, whether a direct comparison is possible and the conclusion should be limited to the general feasibility. Furthermore, it is interesting to note that the debonding mechanisms and hence, the mechanically weakest location in the compound, depends on the frame width. A potential reason for this behavior could be the fact of different forces applied during the bonding process, keeping the contact pressure constant but varying the bonding area.
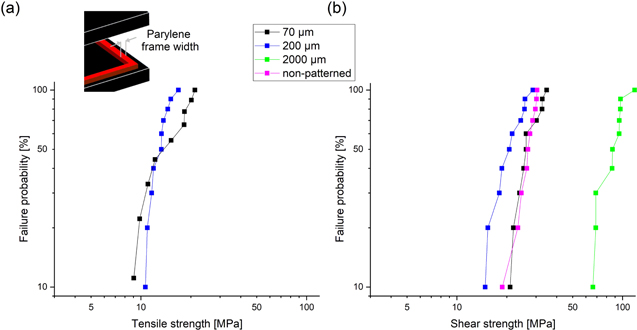
Figure 10. Tensile strength (a) and shear strength (b) of silicon-silicon compounds (Si-P-//-Si) with different parylene frame widths, bonded at a temperature of 280 °C, a contact pressure of 2 bar and a bonding time of 10 min. Note that the tensile strength of the compounds with a frame width of 2000 μm and non-patterned parylene C was not measurable due to failure of the glue. Detailed values are given in Table C·III. 30
Download figure:
Standard image High-resolution imageParylene type
Figure 11 depicts the tensile (a) and shear (b) strengths of the parylene N bonded chips in comparison with parylene C bonded ones. Using parylene N, the bonded wafers were joint inhomogeneously, which was independent of the bonding temperature. Particularly for the results of the mechanical test of the bond performed at 300 °C, a slight tendency was observed with higher strengths at the edge of the wafer when compared to its center. The yield of all parylene N bonded samples was significantly reduced with 78% (250 °C), 70% (280 °C) and 74% (300 °C) compared to 100% for the parylene C references. These results indicate that parylene C can not be simply exchanged by parylene N and the different parylene types require different parameter sets for bonding. Considering the reduced yield, the inhomogeneous joining and the lower mechanical strength of the compounds bonded with parylene N in comparison to the parylene C references, the bonding with parylene N was not successful. Assuming that the adhesive wafer bonding is feasible with parylene N in general and considering that the mechanical strength was almost independent of the bonding temperature, it can be concluded that the optimal bonding temperature is in another temperature range. With respect to the results, it can be assumed that the optimal bonding temperature could be related to the melting temperature of the parylene and not to the duration temperature or temporary peak temperature. In this case, considering the higher melting point of parylene N at 410 °C, 3 its optimal bonding temperature can be expected at higher temperatures compared to parylene C. Considering this and the better material properties of parylene C, it seems less advantageous to exchange parylene C with parylene N or any other parylene type for wafer bonding applications.
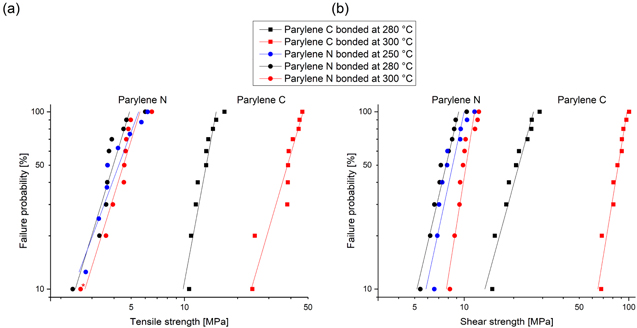
Figure 11. Tensile strength (a) and the shear strength (b) of silicon-silicon compounds (Si–P–//–Si) bonded with different parylene types and at different temperatures. The contact pressure and the bonding time were kept constant at 2 bar and 10 min, respectively. Marks with * indicate glue failure. Detailed values are given in Table C·IV.
Download figure:
Standard image High-resolution imageCross-sectional analysis of the bond interface
The SEM cross-sections of the silicon-silicon compounds (Si–P–//–Si) and the parylene-parylene (Si–P–//–P–Si) bonds are depicted in Fig. 12. The bond interface is verified to be smooth and free of defects such as holes or particles on all images. Furthermore, no indication for the squeezing of the parylene frames was observed from the SEM images, even at higher contact pressures of 3 bar. It is interesting to note that for a parylene-parylene compound bonded at 280 °C (Fig. 12c), still an interface between the two parylene layers is visible (red arrow). According to the SEM images this can be avoided by increasing the bonding temperature to 300 °C and hence, above the melting point. Additional SEM images of the inner area of the bonding frame revealed some cracks. These SEM images can be found in. 30 The described cracks at the inner bonding frame indicate the absence of epoxy, which would stabilize the substrate material during grinding. Hence, these cracks can be interpreted as an indicator for a closed and hermetic parylene frame.
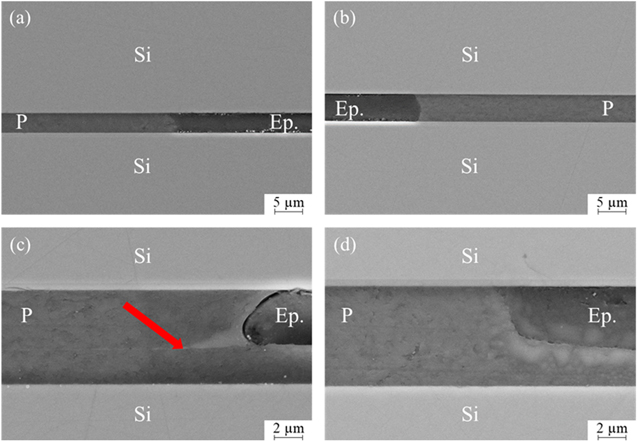
Figure 12. Cross-sectional SEM images of silicon-silicon compounds (Si-P-//-Si) bonded at a temperature and a contact pressure of 280 °C and 2 bar (a) as well as 300 °C and 3 bar (b), respectively. The compounds depicted in (c) and (d) were obtained by bonding against a non-patterned parylene C coating (Si-P-//-P-Si) at a temperature and a contact pressure of 280 °C and 2 bar (c) as well as 300 °C and 2 bar (d), respectively. The samples were embedded into epoxy (Ep.).
Download figure:
Standard image High-resolution imageInfrared light transmission
The images of the wafer compounds captured by IR light transmission are presented in Fig. 13 for a silicon-silicon bond (Si-P-//-Si) with patterned parylene (a) and a compound with non-patterned parylene (b). Due to the particle highlighted in the inset, the yield of this bond was reduced to ∼90 %. The images with patterned parylene revealed that all parylene frames were successfully and homogeneously bonded with a smooth bond interface. Moreover, the area inside and outside the parylene frame remained non-bonded. This is advantageous for the realization of cavities by parylene adhesive bonding. For non-patterned parylene, the analysis with IR light transmission revealed that a homogeneous bond without any defects can be realized as well. However, the bonding with non-patterned parylene seems to be more sensitive to particles.
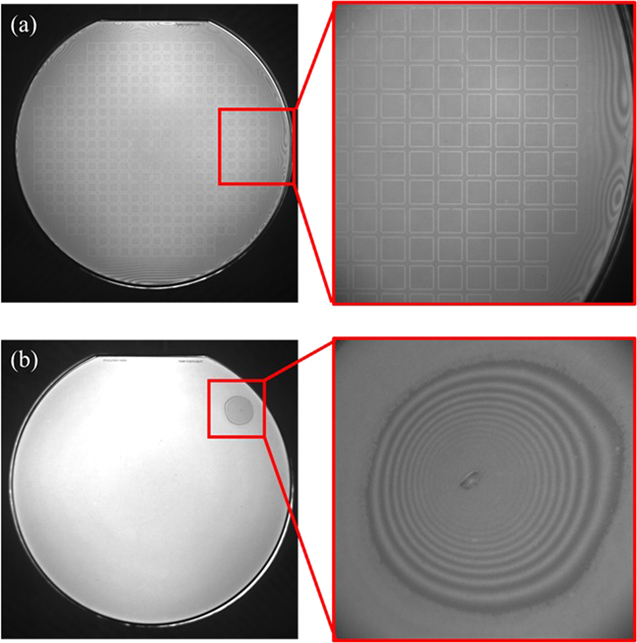
Figure 13. Transmitted IR light images of silicon-silicon (Si-P-//-Si) wafer compounds with patterned parylene C (a) and non-patterned parylene (b).
Download figure:
Standard image High-resolution imageHermeticity
Table III summarizes the time dependent deflection of the silicon membrane over the vacuumed and sealed cavity, measured by white light interferometry. For statistics, each value in the table represents the average of three identical chips. The data revealed that the silicon membrane remains deflected at a constant value over time. Hence, it can be concluded that the vacuum remains intact and no major leakage takes place via the bonding interface.
Table III. Results of the white light interferometric measurements of silicon membrane deflections over a parylene bonded vacuumed cavity.
| Membrane deflection [μm] | ||
|---|---|---|
| Time [days] | Bonded at 280 °C | Bonded at 300 °C |
| 0 | 4.60 ± 0.09 | 4.57 ± 0.12 |
| 10 | 4.52 ± 0.31 | 4.35 ± 0.13 |
| 14 | 4.49 ± 0.09 | 4.54 ± 0.14 |
| 21 | 4.61 ± 0.13 | 4.70 ± 0.11 |
| 27 | 4.60 ± 0.18 | 4.64 ± 0.14 |
| 40 | 4.57 ± 0.13 | 4.69 ± 0.15 |
The results of the helium leakage test are depicted in Fig. 14. Each data point in the diagram was calculated by averaging five samples of the respected sample type. For further consideration, the decrease of the helium leakage rate within the first 30 s was neglected, since it is caused by the rest helium in the air. The helium leakage rate stabilized below 10‒7 mbar∙l/s, which was independent of the bonding temperature. Hence, the parylene bond interface showed a good hermeticity. In particular, for the compounds bonded at 280 °C, a helium leakage rate below 5∙10‒8 mbar∙l/s was measured, which is in accordance with the hermeticity requirements given by MIL-STD-883.
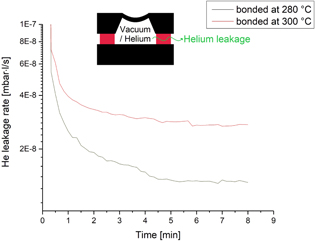
Figure 14. Results of the helium leakage test for the investigation of the hermeticity. 30
Download figure:
Standard image High-resolution imageThe measurements of the −3 dB frequency of the parylene bonded and sealed MEMS acceleration sensor are depicted in Fig. 15. Each data point in the diagram represents the average of three identically treated sensors. The detailed values are summarized in Table B·I in annex B. The reference values of the −3 dB frequency measured on the air damped sensor before bonding at 1 bar atmospheric pressure were in the range between 1670 Hz and 2010 Hz. The grey bar represents the time period for the thermal cycling about three weeks after bonding. The measurements revealed that due to the vacuum caused by the parylene bond, the −3 dB frequency was increased by a factor of 2.5 to 3, compared to the ambient pressure air damped structures. Furthermore, by the higher −3 dB frequency after bonding, it can be concluded that the 200 μm wide parylene bonding frames provide a better hermeticity in comparison to frames of 50 μm width. The decrease of the −3 dB frequency over time indicates a leakage of air into the cavity. However, this leakage is small considering that the −3 dB frequency of the MEMS is also highly sensitive to the smallest change in damping caused by a small change of pressure. After a period of almost one year after bonding, the vacuum is still present, indicated by significant higher values of the −3 dB frequency compared to the air damped sensor. It is interesting to note the effect of the thermal cycling on the hermeticity of the parylene bonding interface: Compared to the samples without thermal cycling, the treated samples feature a lower hermeticity and higher leakage rate, respectively, as it is indicated by a faster decrease of the −3 dB frequency. However, the increased leakage caused by thermal cycling is not a permanent effect. According to the slower decrease of the −3 dB frequency, the leakage was reduced after thermal cycling again so that the −3dB frequency values of the sensor with and without thermal cycling were roughly the same at one year after bonding. In conclusion, the parylene bonding interface provides an excellent and stable hermeticity against gases and is not permanently altered due to thermal cycling.
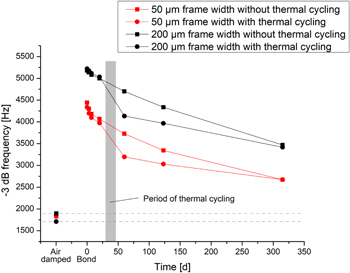
Figure 15. Results of the time depended measurements of the −3 dB frequency of a vacuumed MEMS acceleration sensor sealed by parylene bonding.
Download figure:
Standard image High-resolution imageReliability
Figure 16a depicts the tensile strength of the silicon-silicon (Si-P-//-Si) and silicon-glass (Si-//-P-G) compounds bonded at 280 °C and 300 °C, respectively, before and after thermal cycling. Note that the silicon-glass compounds bonded at 300 C were not measurable in the tensile test due to glue failure. Hence, they were not considered further. An analysis of the fractured surface revealed that the debonding mechanism (adhesive or cohesive) was not influenced due to the thermal cycling. It is interesting to note that for parylene-parylene (Si-P-//-P-Si) bonded samples, which were investigated in parallel, a similar tendency was observed. The measurements show only a limited decrease of the tensile strengths to 60% to 85% of the values without treatment, considering the average tensile strength each. For the decrease of the tensile strength due to thermal cycling, no dependency on the bonded material combination (Si-P-//-Si vs. Si-//-P-G, vs. Si-P-//-P-Si) as well as on the bonding temperature was observed. After the thermal cycling, the previously observed strong influence of the bonding temperature on the tensile strength was still noticeable. Particularly, for the silicon-silicon compounds, the thermally cycled samples bonded at 300 °C still featured a higher tensile strength than the samples bonded at 280 °C before the thermal cycling did. In conclusion, the thermal reliability of the investigated parylene bonds was good.
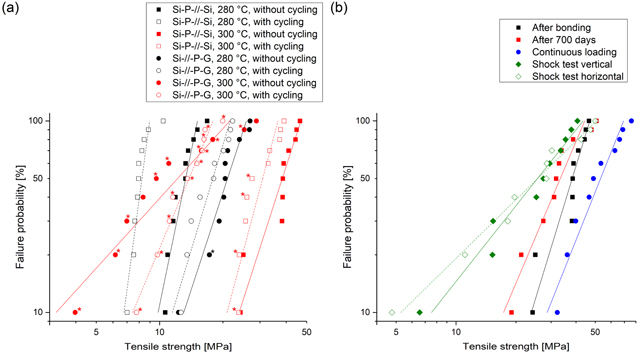
Figure 16. Results for the tensile strength of silicon-silicon (Si-P-//-Si) and silicon-glass compounds (Si-//-P-G) before and after thermal cycling (a) as well as results for the tensile strength of silicon-silicon compounds (Si-P-//-Si) after bonding, after 700 days of aging, after continuous loading and after mechanical shocking (b). Marks with * indicate glue failure. Detailed values are given in Table C·V.
Download figure:
Standard image High-resolution imageFigure 16b summarizes the results of the tensile test for the mechanical reliability testing in the way of continuous load and mechanical shocking in comparison with the values measured directly after bonding and after 700 days of aging. It is interesting to note that the application of the same continuous load to identically processed compounds, which were bonded at 280 °C only, keeping all other parameters the same, failed, even though the load was only about two third of the values obtained by the tensile test. This underlines the lower stability of these compounds bonded at lower temperatures, which was also indicated by the results of the tensile test. The mechanical reliability testing revealed that the application of a continuous load did not influence the tensile strength of the samples negatively. In contrast, their tensile strength even slightly increased. A potential reason for this behavior could be the reorganization of the polymer chains due to slow creeping under the load. The shock test weakened the tensile strength of the bond as it is indicated by a more slanted curve in the Weibull plot and hence, a higher variation of the results. Still, comparing the maximum tensile strength before and after shocking revealed that the weakening of the strength is a statistical process, in which the tensile strength of about 40% of the samples is decreased. In contrast to this, aging for 700 days at ambient conditions only causes a minor decrease of ∼10% of the tensile strength, which is in accordance with literature. 13,15 Hence, in summary it can be concluded that the thermal and mechanical reliability of the parylene bond as well as its stability against aging is good.
Bonding with structures
The SEM images of the cross-sections of the parylene bonded 3D structures are depicted in Fig. 17. Figure 17a represents the bonding against patterned aluminum electrodes of 1 μm height and 200 μm width. Figure 17b represents the realization of a cavity by parylene bonding using its highly conformal deposition. Due to the grinding when preparing the cross-section, the cavity was filled with epoxy (Ep.) particles. However, by IR light transmission it was proved that this is a matter of the sample preparation and such a cavity is empty after bonding. These results demonstrate that the parylene adhesive wafer bonding can be used in different ways for the realization of complex structures: on the one hand side, parylene can be used to level an inhomogeneity. On the other hand side, the highly conformal parylene layer can be used to replicate the coated structure and realize empty cavities without patterning the parylene itself. Additionally, as the previous sections demonstrated by bonding with parylene frames, the parylene can also be patterned to realize cavities and 3D structures. Particularly, this result proved, that other MEMS structures such as movable springs and membranes would not get blocked or stuck during the parylene bonding process. Besides acting as an adhesive, the final function of the parylene layer during bonding depends on its dimensions with respect to the dimensions of the other structures as well as on the process conditions of the bonding process. The compatibility of the parylene compounds with subsequent processes such as grinding and CMP enables the realization of complex MEMS.
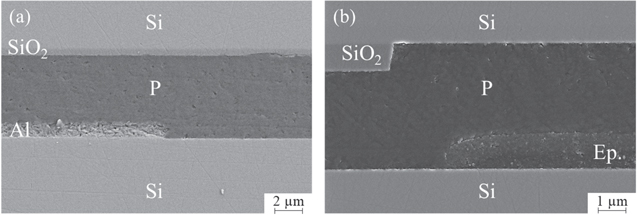
Figure 17. Cross-sectional SEM images of parylene bonded wafer compounds with aluminum electrodes (a) and a silicon dioxide step (b).
Download figure:
Standard image High-resolution imageDiscussion
The presented results mark a major progress of the parylene adhesive wafer bonding compared to the state of the art. 9–20 Within this study, for the first time, the parylene bonding was verified for industry applicable wafer sizes of 150 mm and 200 mm diameter as well as for common materials established in microsystems technology. Besides these established materials it is interesting to highlight the parylene-parylene bonding (e.g. Si–P–//–P–Si), which achieved comparable or even better mechanical strengths than other tested materials. Since parylene can be coated on almost every substrate material and in consideration of the various options for surface pre-treatments such as plasma treatments or adhesion promoters to realize a good adhesion, parylene-parylene bonding can be considered as a general possibility for parylene adhesive bonding of various surfaces. Hence, parylene-parylene bonding could enable also the bonding of surfaces, which cannot be directly bonded or which were not investigated in detail before. Furthermore, the bonding against aluminum was demonstrated for the first time as well. Besides the material related investigations, this study provides a more detailed understanding of the parylene adhesive wafer bonding, investigating the influence of the different process parameters and the parylene dimensions and type on the mechanical strengths of the bond. Doing so, a parameter range for the bonding temperature and time as well as the contact pressure as the most important bonding parameters was identified, in which the mechanical strength of the parylene bonded compound was excellent and significantly higher than given in the literature. For the bonding temperature, a range between 280 °C and 300 °C was identified to produce good results. In comparison to the scientific literature, this range is similar 9,10 or significantly higher. 11–17,19 Only one study is available, which used even higher bonding temperatures. 19 In contrast to the literature, parylene bonding using bonding temperatures of 230 °C and below 11–17 was not considered to be reproducible due to a lower yield. For the first time, it was proven that parylene C is compatible with these temperatures under bonding conditions. In contrast to some processes given in the literature, 10,12,20 the bonding process described in this paper does not require any parylene surface activation by plasma or annealing in air, which avoids the risk of any oxidation, and hence, alteration of the parylene properties. Bonding times typically used in the literature are about 30 min 9–19 or even much longer. 20 Within this study, the feasibility of parylene bonding was demonstrated for significantly shorter bonding times of 10 min and 5 min only, which is advantageous for the use of this process in industry and even caused slightly improved mechanical strengths. With respect to the industry, also the observed yields of 100% are advantageous. Furthermore, the tests with parylene N can be considered as progress compared to the literature, even though parylene N did not produce high mechanical strengths. The best mechanical strength achieved in this study was an average tensile and shear strength of 35 MPa and 80 MPa, respectively, for a parylene bonded silicon-silicon compound (Si-P-//-Si). This result represents an increase of a factor of >3.5 compared to good results given in literature 9,17,18 and an increase of a factor >1.5 compared to the best result given in literature. 10
Additionally, the characterization of the parylene bonded compounds within this study is considered to be a progress with respect to the state of the art. Beside the cross-sectional SEM analysis and the IR light transmission, this particularly refers to the hermeticity and reliability investigations. The hermeticity was characterized in three different ways addressing the exclusion of major leakage, the quantification of the helium leakage with respect to the industry relevant MIL-STD-883 as well as the long-term stability, reliability and applicability for a highly sensitive MEMS acceleration sensor. Each of the three different characterization approaches confirmed the excellent hermeticity of the bond interface. With respect to the reliability, for the first time the thermal and mechanical reliability were investigated and found to be excellent. The results with respect to aging given in the literature were confirmed. 13,15
Finally, a progress with respect to the state of the art is the demonstration of the parylene adhesive wafer bonding for two new applications, which show the potential bandwidth of possible use cases for this technology.
Conclusions
The presented study provided details of the parylene adhesive wafer bonding process with respect to suitable parameter sets, bondable materials as well as suitable parylene dimensions and types. Doing so, a parameter set of a bonding temperature of 280 °C to 300 °C, a bonding time of 5 min to 30 min and a contact pressure of 2 bar to 3 bar was identified to be optimal. It was verified that these process conditions do not negatively influence parylene C. The parylene bonding was successfully demonstrated on wafers with diameters of 150 mm and 200 mm, bonding different material combinations including silicon, glass, silicon dioxide, silicon nitride, aluminum and parylene C. Suitable parylene dimension ranges include thicknesses between 0.5 μm and 10 μm and structure width between 50 μm and non-patterned parylene. It was proven that the parylene type is significant and cannot be exchanged without major impact. The mechanical stability was characterized to be excellent with average values of up to 35 MPa and 80 MPa for the tensile and shear strength, respectively. In particular, the increase of the bonding strength and the bonding of larger wafer sizes are evident for the progress compared to the state of the art. Using the established bonding process for different applications with more than 100 wafers also proves the reproducibility of the results.
The bond interface was characterized by infrared transmission imaging and cross-sectional SEM to be smooth, homogeneous and free of any defects. Different investigations of the hermeticity revealed excellent barrier properties of the parylene bond interface, suitable also for long-term applications. The characterization of different impacts such as thermal cycling, mechanical shocking, continuous loading or aging confirmed the good reliability of the parylene bonded compounds. These investigations mark a major progress compared to the state of the art as well. Finally, two application scenarios were demonstrated for the parylene bonding. In summary, by the investigations, an adhesive wafer bonding process for the joining of 150 mm and 200 mm wafers and the realization of highly reliable and fully biocompatible microsystems was established and characterized.
Acknowledgments
This work has been supported and partially funded by the European Social Fund ESF, the Fraunhofer Society as well as the European Union’s Horizon 2020 research and innovation programme under grant agreement No 732482. Particularly, the authors thank S. Uhlig for bonding the wafers, P. Schwarz for dicing the bonds, C. Hellmann, M. Eichstädt and D. Ullmann for performing the tensile and shear tests, respectively, K. Kreyßig for the thermal cycling of the samples, W. Mende for the measurements at the white light interferometer, R. Kinner for the helium leakage test, M. Rennau for the electrical measurements as well as P. Teicher, S. Rabe and C. Kowol for the preparation of the cross-sections and their investigation in the SEM, respectively. Furthermore, special thank goes to all involved colleagues at the Center for Microtechnologies at the TU Chemnitz for processing the wafers. Additionally, the authors thank all involved colleagues at Fraunhofer Institute for Electronic Nano Systems, the Institute for Electronic and Sensor Materials at TU Bergakademie Freiberg and the Center for Microtechnologies at TU Chemnitz for their support and fruitful discussions. Additional special thanks goes to the colleagues at the Fraunhofer Institute for Photonic Microsystems for the fruitful collaboration dedicated to the parylene bonding of three dimensional structures from which Fig. 17b was created.
Appendix A.: FTIR Spectroscopy
Figure A·1 depicts the process flow for the fabrication of free-standing parylene membranes. A silicon dioxide layer of 500 nm thickness was deposited on a double side polished silicon wafer (1) using thermal oxidation (2). Next, the backside silicon dioxide was patterned using wet etching in hydrofluoric acid and a hard mask of 100 nm silicon nitride. The latter was deposited by low pressure CVD and patterned on the backside using plasma etching in combination with a mask of photo resist. The patterned silicon dioxide was used as a mask for the backside etching of cavities into silicon using potassium hydroxide (3). Subsequent to this, the backside of the wafer was masked and 5 μm parylene C were deposited by CVD (4). Finally, the remaining silicon in the cavity and the front side silicon dioxide were removed by wet chemical etching with potassium hydroxide and hydrofluoric acid, respectively, in order to release the parylene membrane (5).
The fabricated parylene membranes were measured by FTIR before and after annealing. Due to the measurements in transmission mode, the obtained spectra were smoothed by fitting and subtracting a sinus function. The fitting parameters for the sinus function are summarized in Table A·I. The assignment of the peaks in the FTIR spectra with the vibrational modes is given in Table A·II.
Table A·I. Fitting parameters for the sinus function.
| Fit parameters | ||||
|---|---|---|---|---|
| Sample | A [a.u.] | B [cm] | C [a.u.] | D [a.u.] |
| Reference (no annealing) | 0.045 | 0.00820 | 4.80 | 0.270 |
| Annealed at 260 °C | 0.045 | 0.00825 | 4.70 | 0.375 |
| Annealed at 280 °C | 0.044 | 0.00840 | 4.80 | 0.310 |
| Annealed at 300 °C | 0.045 | 0.00810 | 11.00 | 0.295 |
| Annealed at 320 °C | 0.045 | 0.00802 | 4.80 | 0.320 |
Table A·II. Assignment of the FTIR vibrational modes.
| Wave number k [cm−1] | Mode | References |
|---|---|---|
| 826 | H-C-H two neighboring hydrogen atoms bonded to the ring | 25 |
| 826 | C-C aliphatic stretching | 26 |
| 826 | C-H out of plane wagging | 27, 28 |
| 878, 906, 949 | C-H single hydrogen to the ring, out of plane wagging | 25, 27, 28 |
| 1004, 1050 | C-H in-plane bending | 27, 28 |
| 1050 | C-Cl bonding to the ring | 25 |
| 1077, 1110, 1158, 1210, 1267 | CH2 wagging | 27, 28 |
| 1341, 1404, 1495 | C = C semicircle stretching | 27, 28 |
| 1452 | CH2 on the benzene ring | 25 |
| 1452 | CH2 deformation | 27, 28 |
| 1493 | C-C aromatic stretching | 26 |
| 1558, 1610 | C = C ring stretching | 27, 28 |
| 1700 | Parylene oxidation (C = O stretching) | 27–29 |
| 2865, 2928 | C-H aliphatic stretching | 25–28 |
| 3020 | C-H aliphatic stretching | 27, 28 |
| 3020 | C-H aromatic stretching | 25, 26 |
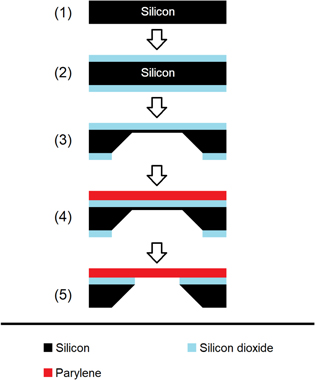
Figure A·1. Schematic process flow for the preparation of free-standing parylene membranes used for FTIR analysis. Note that the graphic is not to scale.
Download figure:
Standard image High-resolution imageAppendix B.: Hermeticity of Parylene Acceleration Sensor
Table B·I. −3 dB frequencies of a vacuumed MEMS acceleration sensor sealed by parylene bonding.
| −3 dB frequency [Hz] | ||||
|---|---|---|---|---|
| 50 μm parylene frame width | 200 μm parylene frame width | |||
| Without thermal cycling | Thermal cycling | Without thermal cycling | Thermal cycling | |
| Air damped | 1827 ± 124 | 1853 ± 172 | 1895 ± 64 | 1710 ± N/A |
| Bonded | 4443 ± 251 | 4337 ± 526 | 5180 ± 72 | 5220 ± 234 |
| 3 days | 4300 ± 231 | 4197 ± 526 | 5137 ± 68 | 5173 ± 237 |
| 7 days | 4183 ± 250 | 4097 ± 501 | 5083 ± 74 | 5117 ± 240 |
| 20 days | 4067 ± 251 | 3973 ± 501 | 5000 ± 78 | 5033 ± 263 |
| 60 days | 3727 ± 267 | 3197 ± 427 | 4700 ± 104 | 4133 ± 238 |
| 123 days | 3343 ± 269 | 3030 ± 409 | 4337 ± 95 | 3967 ± 320 |
| 315 days | 2670 ± 225 | 2673 ± 341 | 3470 ± 135 | 3417 ± 359 |
Appendix C.: Values for the Bonding Strength
Table C·I. Results for the bonding strengths for bonding parylene C with different parameter sets. Italic values mark glue failure.
| Tensile strength [MPa] | Shear strength [MPa] | ||||||
|---|---|---|---|---|---|---|---|
| Bonding parameters | 20% failure | 50% failure | 80% failure | 20% failure | 50% failure | 80% failure | |
| Contact pressure | |||||||
| Si-P-//-Si, 10 min / 300 °C bonding time / temperature | 1 bar | 4.55 | 5.46 | 9.08 | 57.35 | 61.98 | 65.01 |
| 2 bar | 25.02 | 38.54 | 44.26 | 68.69 | 85.42 | 92.75 | |
| 3 bar | 42.09 | 46.80 | 54.00 | 67.02 | 70.97 | 72.93 | |
| Bonding temperature | |||||||
| 10 min bonding time, 2 bar contact pressure | Si-P-//-Si | ||||||
| 260°C | 6.21 | 7.68 | 10.02 | 12.57 | 14.03 | 20.16 | |
| 280°C | 10.92 | 13.28 | 14.51 | 15.37 | 20.68 | 25.60 | |
| 300°C | 25.02 | 38.54 | 44.26 | 68.69 | 85.42 | 92.75 | |
| Si-//-P-G | |||||||
| 260°C | 12.83 | 14.05 | 16.20 | 13.57 | 15.03 | 16.89 | |
| 280°C | 17.25 | 20.50 | 23.96 | 26.28 | 27.94 | 35.26 | |
| 300°C | 6.16 | 9.66 | 17.90 | 59.58 | 68.17 | 69.69 | |
| Bonding time | |||||||
| Si-P-//-Si, 2 bar contact pressure, 280 °C bonding temperature | 5 min | 11.81 | 12.93 | 15.96 | 19.56 | 20.74 | 26.17 |
| 10 min | 10.92 | 13.28 | 14.51 | 15.37 | 20.68 | 25.60 | |
| 30 min | 7.43 | 9.47 | 13.14 | 9.47 | 13.55 | 16.67 | |
Table C·II. Results for the bonding strengths for bonding parylene C with different material combinations. Italic values mark glue failure.
| Tensile strength [MPa] | Shear strength [MPa] | ||||||
|---|---|---|---|---|---|---|---|
| Bonding parameters and materials | 20% failure | 50% failure | 80% failure | 20% failure | 50% failure | 80% failure | |
| Bonding at 280 °C | |||||||
| Si-P-//-Si | 10.92 | 13.28 | 14.51 | 15.37 | 20.68 | 25.60 | |
| Si-//-P-G | 17.25 | 20.50 | 23.96 | 26.28 | 27.94 | 35.26 | |
| Si-P-//-SiO2-Si | 10.76 | 11.94 | 14.27 | 19.97 | 20.46 | 22.13 | |
| Si-P-//-SiNx-Si | 6.25 | 9.79 | 10.82 | 22.20 | 23.40 | 24.54 | |
| Si-P-//-Al-Si | 9.20 | 10.12 | 12.13 | 10.93 | 13.47 | 19.31 | |
| Si-P-//-P-Si | 10.55 | 12.50 | 13.83 | 20.03 | 20.98 | 23.50 | |
| 10 min bonding time, 2 bar contact pressure | Bonding at 300 °C | ||||||
| Si-P-//-Si | 25.02 | 38.54 | 44.26 | 68.69 | 85.42 | 92.75 | |
| Si-//-P-G | 6.16 | 9.66 | 17.90 | 59.58 | 68.17 | 69.69 | |
| Si-P-//-SiO2-Si | 17.43 | 31.94 | 35.52 | 69.47 | 75.61 | 78.56 | |
| Si-P-//-SiNx-Si | 24.73 | 25.20 | 34.15 | 69.49 | 72.81 | 77.83 | |
| Si-P-//-Al-Si | 26.42 | 35.00 | 38.45 | 75.47 | 78.89 | 84.37 | |
| Si-P-//-P-Si | 19.67 | 31.19 | 41.38 | 92.45 | 97.88 | 99.79 | |
Table C·III. Results for the bonding strengths for bonding parylene C with different geometries. Italic values mark glue failure.
| Tensile strength [MPa] | Shear strength [MPa] | ||||||
|---|---|---|---|---|---|---|---|
| Bonding parameters | 20% failure | 50% failure | 80% failure | 20% failure | 50% failure | 80% failure | |
| Parylene frame thickness | |||||||
| Bonding at 280 °C | |||||||
| 10 min bonding time, 2 bar contact pressure | 5 μm | 17.25 | 20.50 | 23.96 | 26.28 | 27.94 | 35.26 |
| 10 μm | 5.02 | 6.27 | 11.12 | 10.00 | 17.66 | 19.92 | |
| Bonding at 300 °C | |||||||
| 5 μm | 6.16 | 9.66 | 17.90 | 59.58 | 68.17 | 69.69 | |
| 10 μm | 16.05 | 20.36 | 27.66 | 67.32 | 71.16 | 76.02 | |
| Parylene frame width | |||||||
| 70 μm | 9.05 | 12.17 | 18.30 | 21.93 | 26.16 | 32.64 | |
| 10 min / 280 °C bonding time / temperature, 2 bar contact pressure | 200 μm | 10.92 | 13.28 | 14.51 | 15.37 | 20.68 | 25.60 |
| 2000 μm | 1.66 | 3.37 | 4.29 | 68.88 | 86.90 | 97.00 | |
| Non-patterned | 2.49 | 3.30 | 5.06 | 23.32 | 26.84 | 29.78 | |
Table C·IV. Results for the bonding strengths for bonding different parylene types.
| Tensile strength [MPa] | Shear strength [MPa] | ||||||
|---|---|---|---|---|---|---|---|
| Bonding parameters | 20% failure | 50% failure | 80% failure | 20% failure | 50% failure | 80% failure | |
| 10 min bonding time,2 bar contact pressure | Parylene C | ||||||
| 280 °C | 10.92 | 13.28 | 14.51 | 15.37 | 20.68 | 25.60 | |
| 300 °C | 25.02 | 38.54 | 44.26 | 68.69 | 85.42 | 92.75 | |
| Parylene N | |||||||
| 250 °C | N/A | 3.65 | 4.91 | 6.87 | 7.87 | 9.52 | |
| 280 °C | 3.31 | 3.67 | 4.53 | 6.22 | 7.22 | 8.71 | |
| 300 °C | 3.60 | 4.57 | 4.82 | 8.76 | 9.84 | 11.64 | |
Table C·V. Results for the bonding strengths for different reliability characterizations. Italic values mark glue failure.
| Tensile strength [MPa] | ||||||
|---|---|---|---|---|---|---|
| Bonding parameters / sample description/reliability testing | 20% failure | 50% failure | 80% failure | |||
| Thermal cycling | ||||||
| 10 min bonding time, 2 bar contact pressure | Si-P-//-Si | bonded at 280 °C | w/o cycling | 10.92 | 13.28 | 14.51 |
| Si-P-//-Si | bonded at 280 °C | w cycling | 7.52 | 7.95 | 8.45 | |
| Si-P-//-Si | bonded at 300 °C | w/o cycling | 25.02 | 38.54 | 44.26 | |
| Si-P-//-Si | bonded at 300 °C | w cycling | 23.91 | 27.50 | 37.23 | |
| Si-//-P-G | bonded at 280 °C | w/o cycling | 17.25 | 20.50 | 23.96 | |
| Si-//-P-G | bonded at 280 °C | w cycling | 13.51 | 18.07 | 21.31 | |
| Si-//-P-G | bonded at 300 °C | w/o cycling | 6.16 | 9.66 | 17.90 | |
| Si-//-P-G | bonded at 300 °C | w cycling | 9.77 | 13.56 | 16.27 | |
| Mechanical reliability | ||||||
| 10 min bonding time,/300 °C bonding temperature, 2 bar contact pressure | After bonding | 25.02 | 38.54 | 44.26 | ||
| After 700 days | 21.23 | 31.81 | 38.73 | |||
| Continuous loading | 36.16 | 48.97 | 66.26 | |||
| Shock test vertical | 15.22 | 27.44 | 35.47 | |||
| Shock test horizontal | 11.09 | 28.42 | 42.45 | |||


